Colour is where more bedding orders fall apart than anywhere else. You get the sample looking spot-on in the office, then the bulk shipment arrives a shade off — darker or lighter — and suddenly everyone’s debating whether it’s “close enough.” By that point the fabric’s already dyed or printed, cut and sewn. Remaking it means missing a whole season.
Most of these headaches are totally avoidable. They come from signing off on the wrong thing, under the wrong light, against a reference that was never sharp to begin with. This guide walks you through managing colour matching for both dyed and printed bedding — from that first lab dip all the way to repeat orders twelve months down the line.
Why Colour Drifts Between Lab, Sample and Bulk
A lab dip is just a small swatch of fabric dyed or printed under tight controls. Bulk? That’s a different machine, a different fabric lot, probably a different week entirely. Five things mess it up most of the time:
- The base fabric. Fibre type, yarn count, weave structure, whiteness — all of these change how a colour actually reads. Run the same recipe on a brighter base and it’ll look lighter. Period.
- The dye or ink lot. Suppliers’ lots drift slightly, even when they’re supposed to match the same reference.
- Process parameters. Temperature, time, liquor ratio, paste viscosity, steamer conditions, curing — any one of these shifting will move the shade.
- Washing, softening, calendering — these all change the surface look and depth.
- Judging colour on a phone screen or under office fluorescents isn’t really judging colour at all.
| منصة | What can change | What to control |
| Lab dip to bulk | Base lot, dye lot, liquor ratio, temperature and time | Same base quality, recorded recipe, retained dye lot |
| Artwork to print | Ink limits, colour profile, fabric absorbency | Proof on the production base, not paper |
| Print to finished | Fixation, washing, curing | Locked process parameters, wash test on the finished piece |
| Finished to approval | Light source, background, screen | Physical standard, D65 and store-light viewing |
Set the Colour Standard Before Anything Else
A colour standard is a number plus a physical sample — not a name. “Sage green” means absolutely nothing across a supply chain. A Pantone TCX code plus a sealed swatch? That means the same thing in every factory on the planet.
Four rules keep the standard actually usable:
- Use textile references. Pantone TCX is the textile system. TPX is for paper and won’t match on fabric — don’t mix them up.
- One code per colour. Got four colours in your design? You need four references. Gradients need a defined start and end point, too.
- Keep two sealed standards. One for the buyer, one for the factory. Store them dark, dry, flat. Once a standard fades, it’s no good as a standard anymore.
- Write the tolerance down. Agree on a numeric acceptance range before you even start sampling. That way approval is a measurement, not somebody’s opinion.
| تسامح | What it covers | Common working value |
| Lab dip vs reference | Recipe direction before bulk | ΔE ≤ 1.0 |
| Bulk vs approved standard | Production consistency | ΔE ≤ 1.5–2.0 |
| Batch to batch | Repeat orders | Agree per programme and record it |
| Visual check | Metamerism and appearance | Pass under D65 and TL84 |
Those numbers above? They’re common industry targets, not some universal law. The real key is agreeing on the number with your supplier in writing before the first bulk run.
Judge Colour Under the Right Light
Here’s the thing: two fabrics can match perfectly under one light and look completely different under another. That’s metamerism. It’s exactly why a colour that looked fine when approved in the factory office ends up looking wrong on the retail floor.
- Judge under D65 (noon daylight simulation) as your primary condition. Always.
- Check again under TL84 (retail store lighting). Don’t skip this step.
- For home textiles, throw in a warm domestic light check as a useful third look.
- Same angle, same background, viewing booth. Never — I repeat, never — approve from a photo on a monitor.
| Light source | Simulates | When to use |
| D65 | Noon daylight | Primary approval |
| TL84 | Retail store lighting | Secondary approval |
| Warm white / incandescent | Home lighting | Optional check for bedding and table linen |
| UV | Optical brighteners | Only when the fabric contains brighteners |
Dyed and Printed Colours Fail in Different Places
These two routes need different controls. A buyer who treats them the same will end up approving the wrong sample — and we’ve all seen how that plays out.
Dyed Bedding: Dye Lot and Levelness
When you’re dyeing, the colour gets built right into the fabric. The main risks? The dye lot itself and how even the bath is.
- Approve a lab dip first, then a bulk dye lot sample. Not the other way around.
- Check selvedge to centre and end to end. A shade that drifts across the width will show up ugly at a seam.
- Record the dye lot for every single batch. When you reorder, that previous lot becomes your reference.
- Confirm the shade after washing, not just before. Some dyes shift in the first wash and you don’t want surprises.
Printed Bedding: Profile, Paste and Fixation
With printing, the colour sits on top of the fabric. Every route shifts things differently.
- Digital printing: the colour profile, ink limit and fabric pre-treatment are what decide the result. A proof on paper tells you zip about how it’ll look on cotton sateen.
- Reactive printing: paste formulation, steaming and washing all move the shade. The deepest colours are the least forgiving — they’ll show every mistake.
- Pigment printing: the binder and curing temperature affect both colour and hand feel. Over-cure and whites turn yellow. Under-cure and you lose fastness.
- Screen printing: paste viscosity, squeegee pressure and repeat registration matter way more than the artwork file itself.
| Route | Where colour shifts | What to approve |
| Reactive dyeing | Dye lot, temperature and time, washing | Bulk dye lot sample, washed |
| Pigment dyeing or printing | Binder ratio, curing temperature | Cured finished sample |
| الطباعة الرقمية | Profile, ink limit, pre-treatment | Strike-off on the production base |
| Reactive print | Paste, steaming, washing | Washed finished sample |
| Screen print | Paste viscosity, squeegee, registration | First-off from the production line |
The Approval Chain That Prevents Bulk Disputes
Approving a loose swatch causes more losses than pretty much any other single mistake. Colour moves during printing and fixation, then moves again in the first wash. What you sign off on needs to be an actual finished piece — not an intention.
Here’s a sequence that actually works:
- Hand samples in light, mid and deep. Pick the depth first — it’s way harder to change later than the hue.
- Sample on the production base. A different base will drift, even if you use the same recipe.
- Finish the sample the way bulk will be finished. Print it, fix it, wash it, dry it — the whole deal.
- Wash it once. Check colour, shrinkage and hand feel all together.
- Approve the full width on wide fabric. Edge-to-centre variation is normal — a narrow strip just hides it.
- Photograph the pre-production sample beside the approved standard before anyone starts cutting.
- Seal and file the approved sample. Every reorder gets compared against it.
| خطوة | Deliverable | Sign-off criterion |
| 1 | Hand samples, three depths | Depth selected |
| 2 | Sample on production base | Base confirmed |
| 3 | Finished and washed sample | Colour, shrinkage, hand feel pass |
| 4 | Full-width approval | No visible edge-to-centre shift |
| 5 | Pre-production photograph | Matches sealed standard |
| 6 | Sealed standard filed | Reorder reference agreed |
Holding Colour Across Repeat Orders
The second order is where colour programmes usually go off the rails. The base fabric might come from a different lot. The dye supplier may have changed. The factory might have tweaked its process. You name it.
- Keep the sealed standard and the dye lot record for every batch. No exceptions.
- Specify the same base quality and the same route on the reorder.
- Re-approve if the base whiteness changes. A brighter base reads lighter with the same recipe — it’s basic physics.
- Check the first metres of a new batch against the standard before cutting.
- Treat gaps of six months or more as a brand new colour approval, not a repeat. Don’t assume.
Measuring and Documenting Colour
Visual judgement is necessary but it’s not enough on its own. Instrumental measurement is what makes the difference actually discussable.
- A spectrophotometer gives you a numeric reading — usually ΔE — which tells you the size of the colour difference, not the direction.
- Combine the instrument reading with a visual check under D65 and TL84. A number can pass while the fabric still looks wrong in a real room. Always trust your eyes too.
- Record the reading for each batch, along with the light source and standard used.
- Photograph each batch beside the sealed standard under consistent lighting, with a grey card in the frame.
- Keep the records with the order file. That’s what makes a claim actually resolvable.
HSC Textile runs quality control from raw material all the way to finished goods: pre-production sample approval, checks during cutting and stitching, and final inspection before packing. Production is OEKO-TEX STANDARD 100 certified. Now, OEKO-TEX covers safety — not shade. Colour still needs its own standard and approval record.
The Spec Sheet That Prevents Arguments
Most colour disputes trace back to one missing line on the spec sheet. Here are the fields worth filling in before you even send a quote:
| Field | Example | لماذا يُعد ذلك مهماً؟ |
| Item and finished size | Duvet cover 200 × 200 cm + 2 pillowcases | Repeatability across orders |
| القماش الأساسي | 100% cotton sateen, 300T, bleached white | The base decides the final shade |
| مرجع الألوان | Pantone TCX 19-5217 | Removes ambiguity from colour names |
| Route | Reactive dye / digital print | Different control points per route |
| Placement and repeat | 32 cm repeat, centred, direction marked | Matching at seams and on the bed |
| تسامح | ΔE ≤ 1.5 bulk vs standard | Objective acceptance criterion |
| Light sources | D65 + TL84 | Metamerism check |
| Care label and packaging | Artwork reference attached | Compliance and presentation |
| خطة الكمية وإعادة الطلب | 100 sets, reorder expected in Q2 | Production and lot planning |
Colour Matching in HSC Textile’s Production
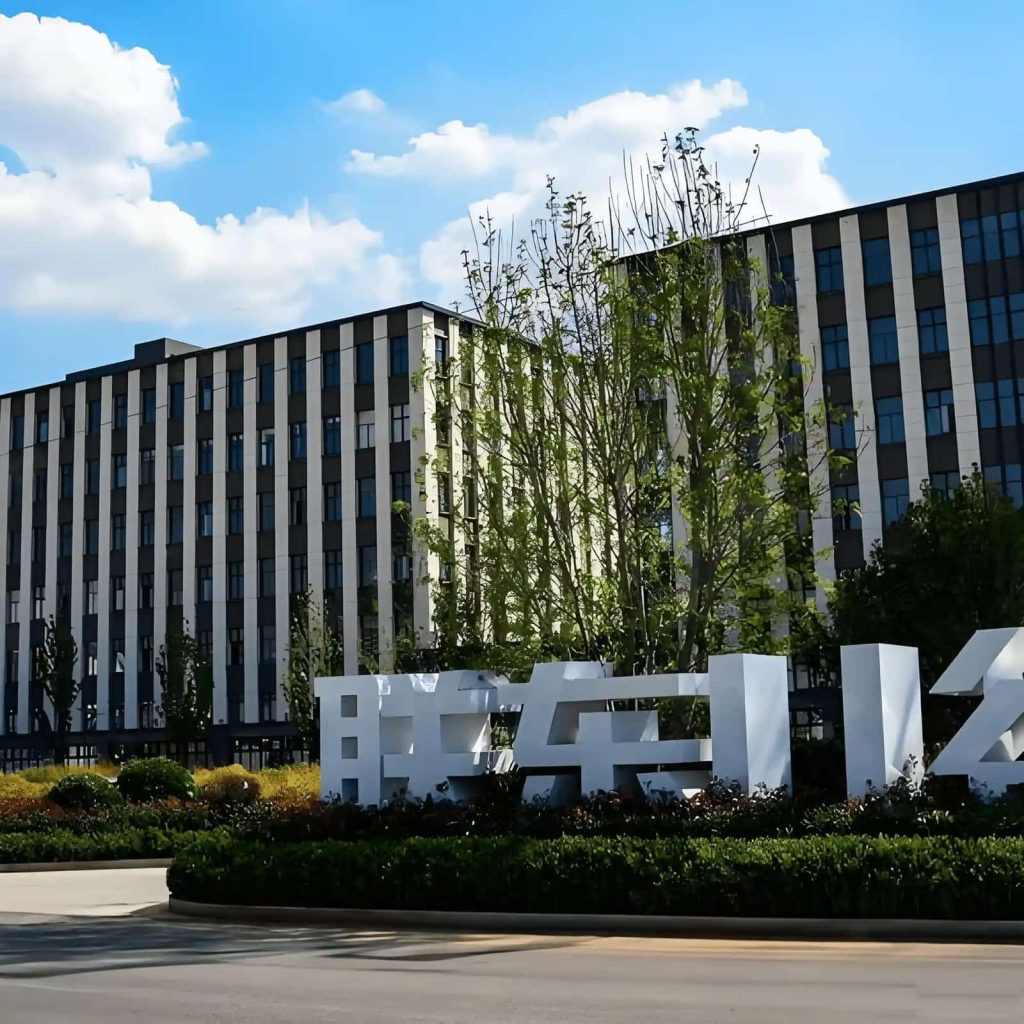
HSC Textile is part of ULAND GROUP — one roof, manufacturing and trading under the same umbrella. Twenty years in home textiles. A 3,200 square meter factory. 55 staff. Clients in more than 30 countries. Printing, dyeing, cutting, stitching and packing all happen in-house. That keeps the colour standard in one place instead of bouncing between several suppliers.
Bedding programmes that depend on colour consistency usually kick off here:
- طقم غطاء لحاف من الساتان القطني العضوي — flat, consistent surface for both dyeing and print.
- طقم مفروشات من الليوسيل المصنوع من الخيزران — a base that shows shade differences clearly, so approval discipline really matters.
- طقم ملاءات سرير قطنية موسلين — gauze texture that softens fine linework.
- Stone-washed French linen duvet cover set — washed finish that shifts shade slightly by design.
Got print-specific questions? Our guide to custom digitally printed bed linen covers routes, artwork and sampling. Browse our أغطية الفراش, أغطية سرير قطنية, أغطية سرير من ألياف الخيزران والليوسيل و مفروشات من القطن العضوي المغسول بالحجر collections. Colour development, sizes, labels and packaging all sit inside the برامج التصميم والتصنيع الأصليين/التصنيع الأصلي للمعدات.
الأسئلة الشائعة
Q1: Why does bulk colour differ from the lab dip?
A: The base lot, dye lot and process conditions all change between a lab dip and bulk. The fix is procedural: sample on the production base, approve a finished and washed piece, and seal the standard that bulk is measured against.
Q2: What is ΔE, and what tolerance should we ask for?
A: ΔE is a numeric measure of colour difference. Common working targets are around ΔE ≤ 1.0 for a lab dip and ΔE ≤ 1.5–2.0 for bulk against the approved standard. Agree the number in writing before production starts.
Q3: What is metamerism, and how do we check for it?
A: Metamerism is when two colours match under one light and differ under another. Check the sample under D65 daylight and TL84 store lighting before approving. Don’t skip either.
Q4: Can you match a Pantone reference on both dyed and printed bedding?
A: Yes. Dyed programmes are matched through a lab dip, printed programmes through a strike-off on the production base. Both are approved as finished, washed samples rather than loose swatches.
Q5: How do you keep repeat orders consistent?
A: Keep a sealed standard and dye lot record for each batch, specify the same base and route, and check the first metres of a new batch. If the base whiteness changes, re-approve the colour. Simple as that.
نبذة عن شركة HSC للمنسوجات
We are ULAND GROUP — a group company integrating manufacturing and trade. Our subsidiaries include HSC, Liaocheng Shanlian Textile Co., Ltd., Zhongfei, and DDL. Got a colour-critical bedding programme? Send over the base fabric, colour references, route, tolerance and quantity, and the team will come back with a sampling and approval plan.